
Dairy — flavoured milk
Flavoured milk
powder systems.
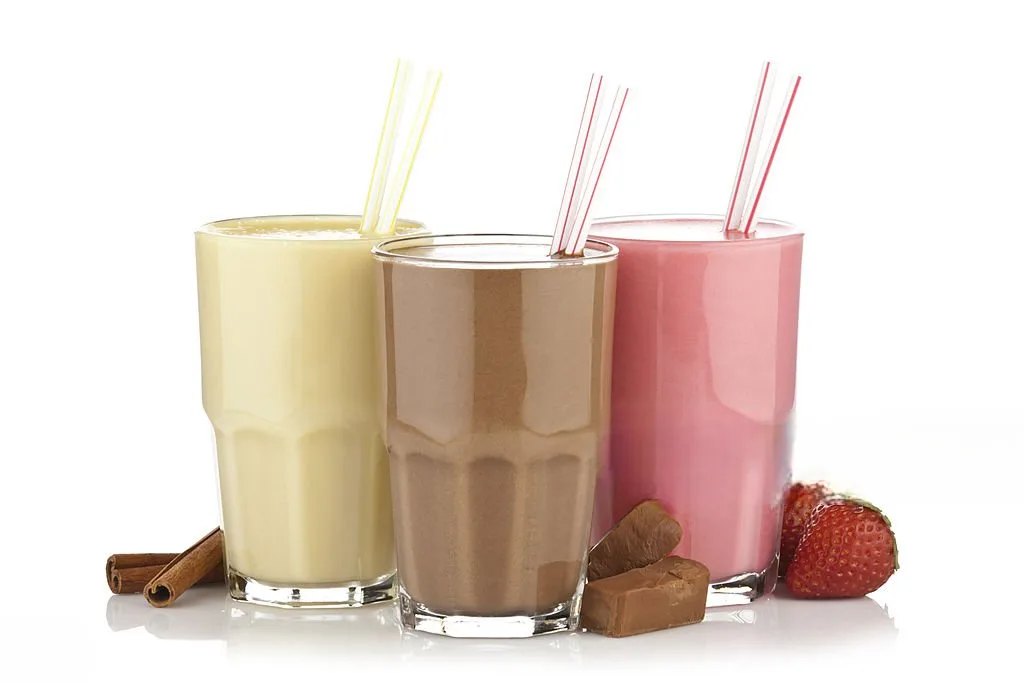
Cocoa, sugar, stabilisers and flavours, dosed into a liquid process — the powder side of a beverage plant, done without the haze.
In brief
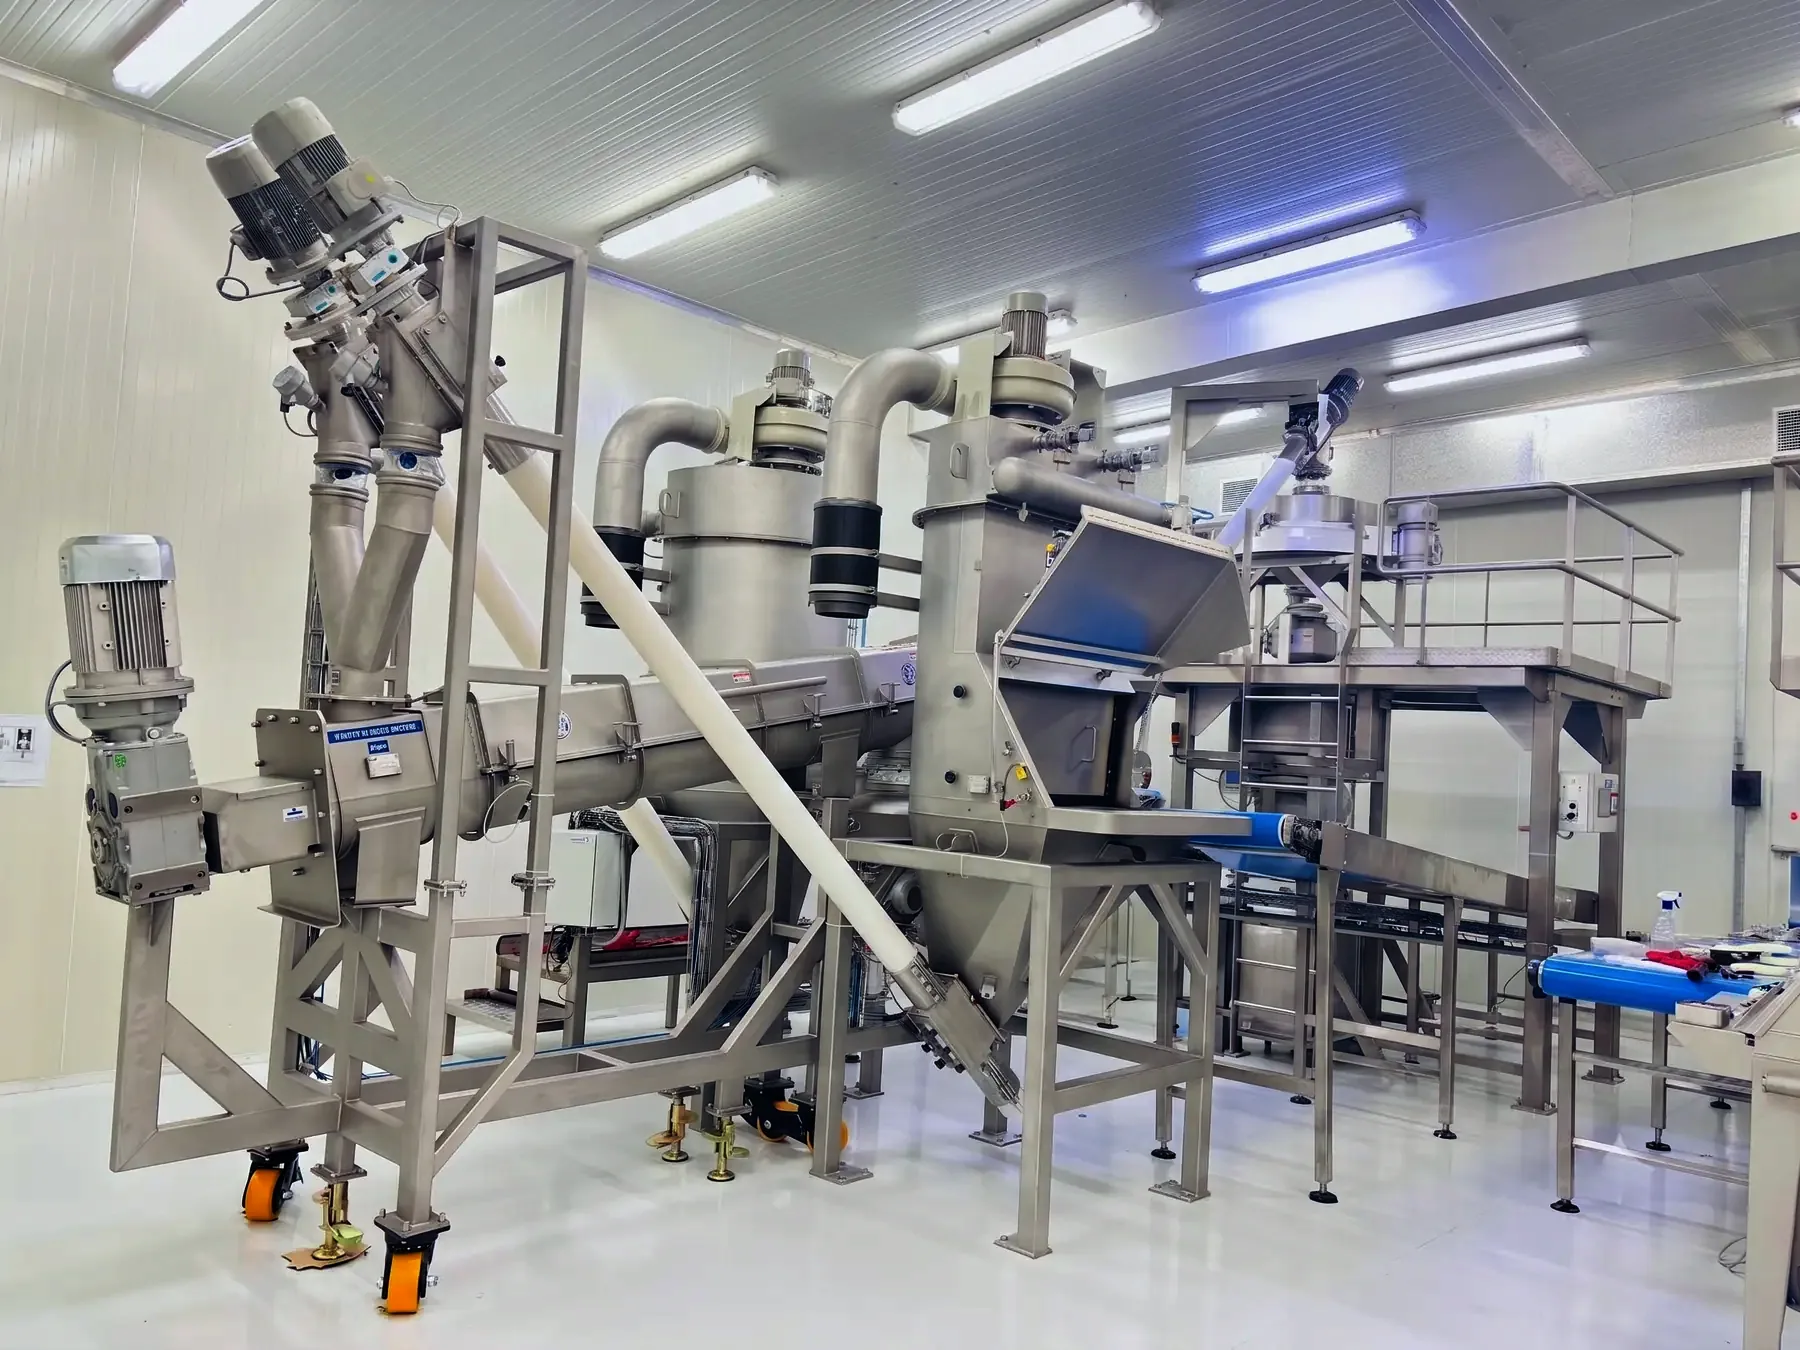
Flavoured milk production doses powders — cocoa, sugar, stabiliser and flavour systems — into liquid processing. TLG builds the powder side: contained intake from bags and bulk bags, weighed batch dosing into mixing vessels, and dust extraction at every transfer, so the powder room stays as clean as the liquid one.
The powder problem
Process requirements.
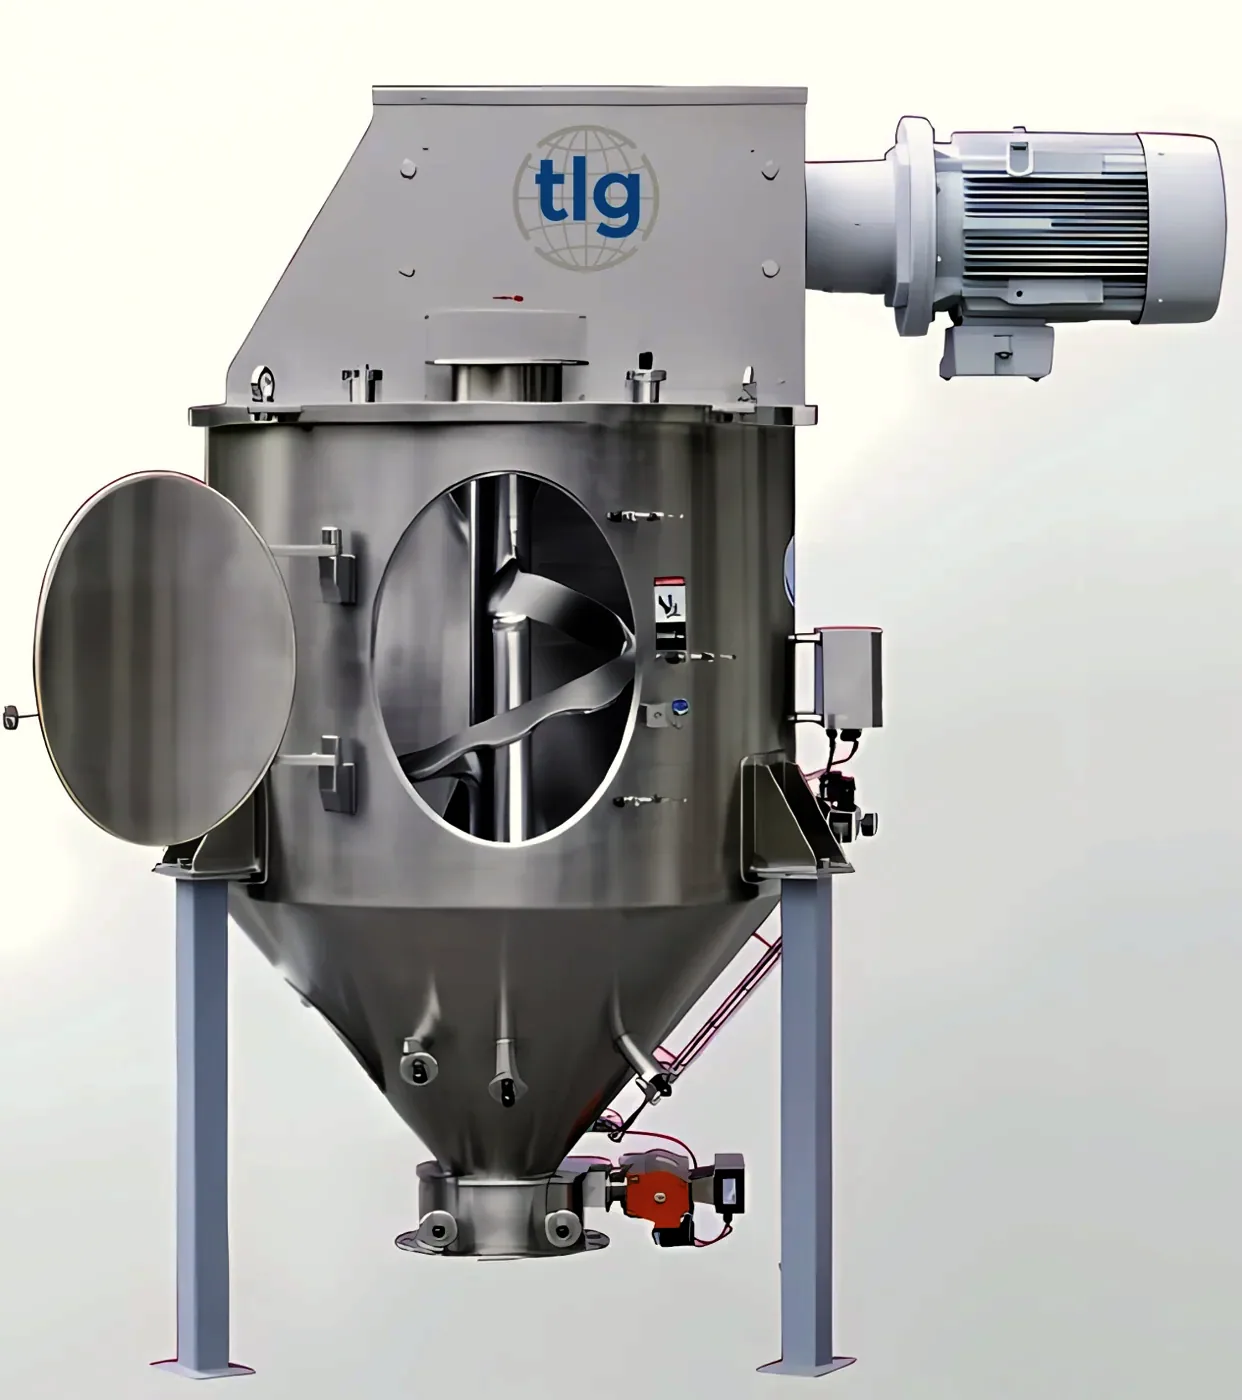
The interface is the design problem: powder must meet liquid at the rate the mixer can wet it, without dusting the room or bridging in the feed. Weighed hoppers above inline mixers, vibratory dosing for clean cut-off, and extraction hoods at the tip points make the transfer routine.
- Powders
- Cocoa · sugar · stabilisers · flavour systems
- Intake
- Bag tip and bulk bag stations, dust-extracted
- Dosing
- Weighed batch delivery into liquid mixing
- Hygiene
- Beverage-grade stainless, wash-down design
The process — stage by stage
The flavoured milk line, stage by stage.
Every stage below is equipment TLG designs and builds — follow any of them into the solutions range.
- 01
Raw material intake
Sacks and bulk bags enter the line contained — dust captured at the tip point, foreign objects screened out.
- 02
Conveying
Transfer matched to the powder — pneumatic phase chosen for friability, mechanical for short controlled runs.
- 03
Raw material & finished goods storage
Silos with discharge engineered to the powder's measured flow properties — storage that empties reliably.
- 04
Automated batching
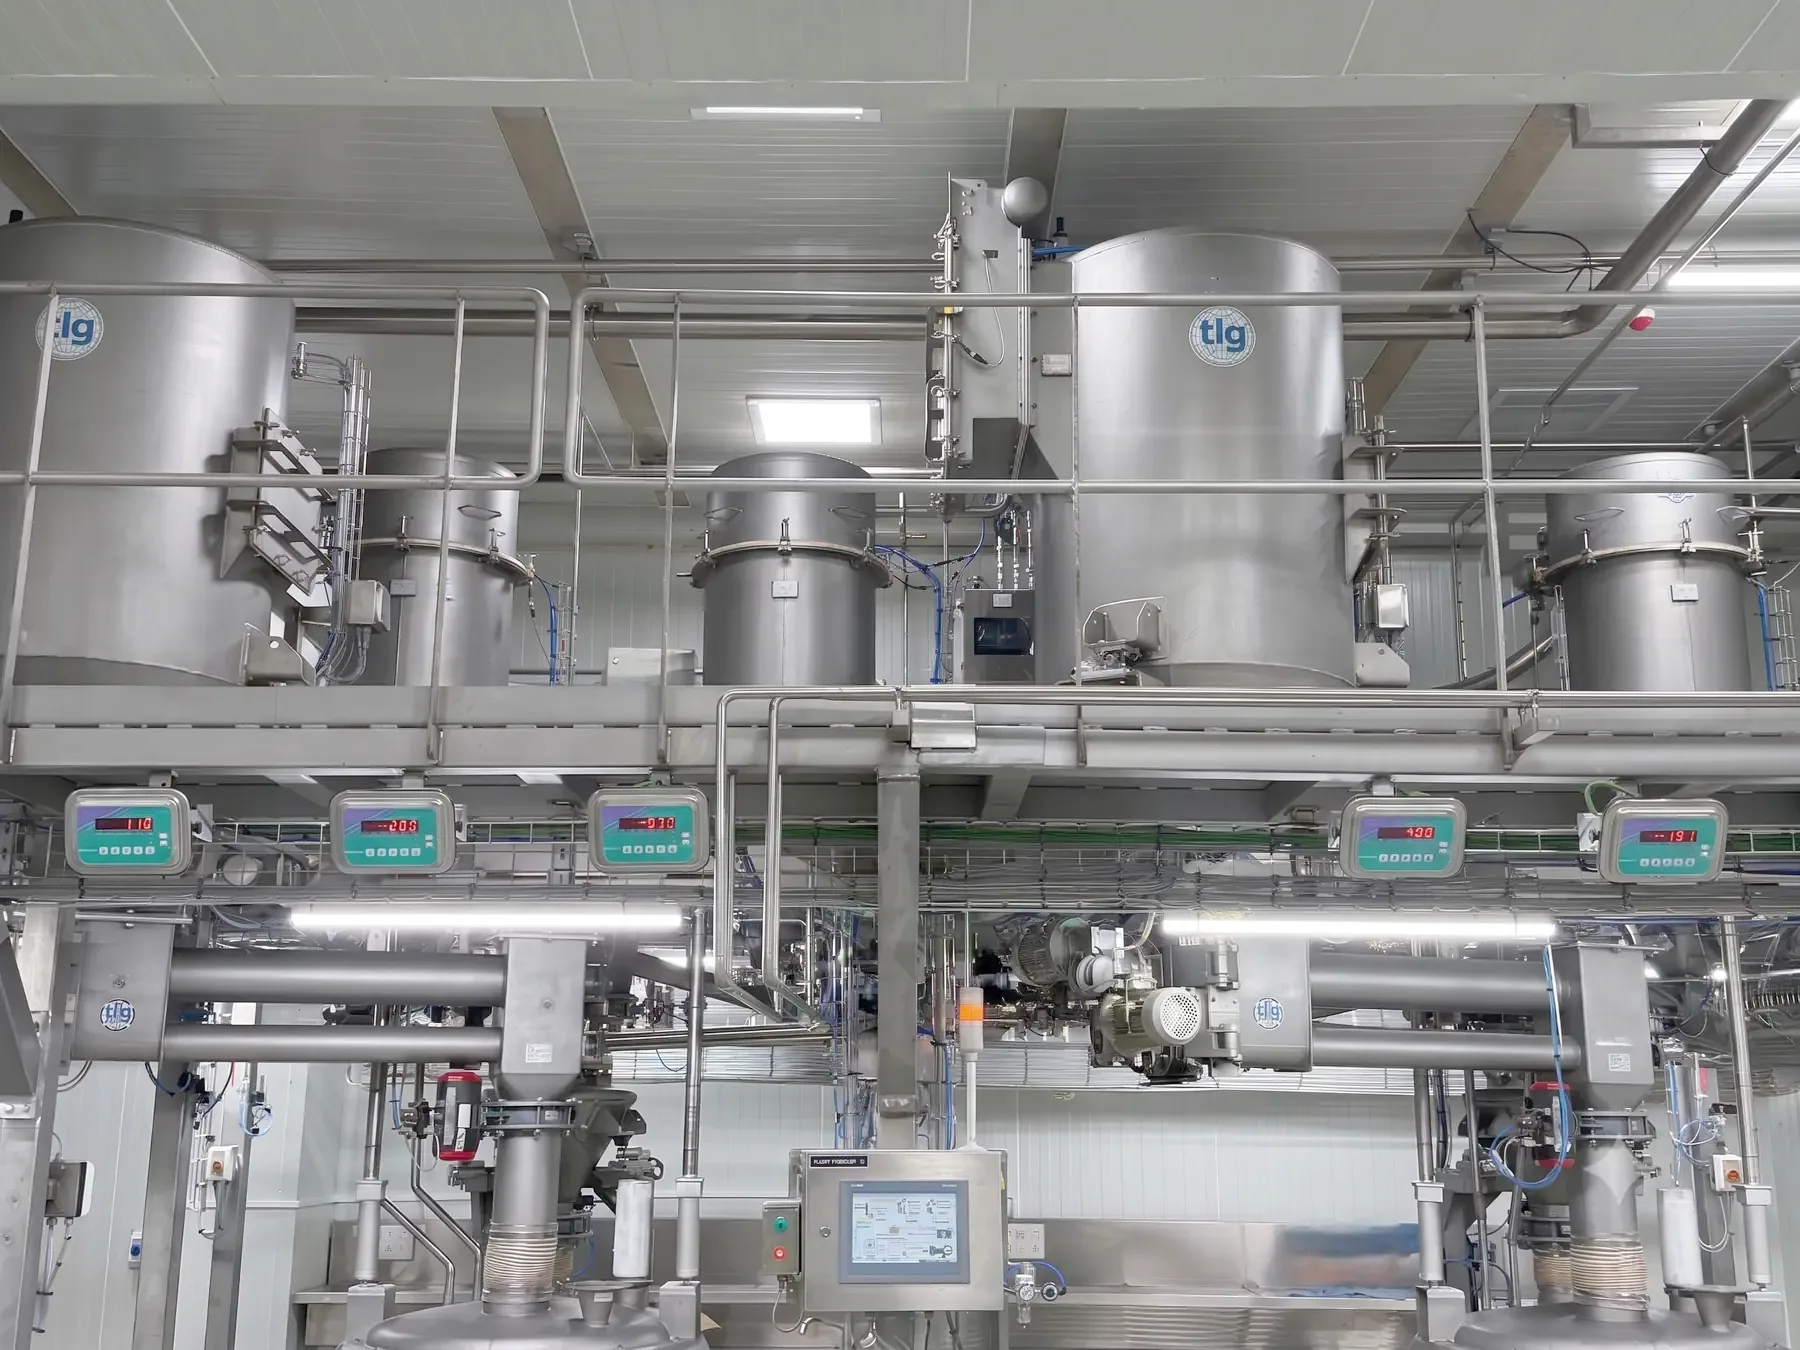
Every ingredient weighed to recipe on isolated load cells, majors to minors, with the batch record generated automatically.
- 05
Foreign material removal
Magnets hold ferrous wear metal; check-sieves reject oversize — placed where HACCP analysis puts them.
- 06
Dust extraction
Capture at every transfer point, ducted to reverse-jet filtration — hygiene, compliance and recovered product.
- 07
Automation & controls
One control system sequencing the whole line — recipes, interlocks and records included.
Related
Related pages.
Discuss your project.
Talk to an engineer.
Send the material, throughput and plant constraints. You’ll get a considered answer from an engineer, not a brochure.